How to Ensure China Medical Suppliers Meet Global Standards?

Time:2026-09-27 Author:Amelia
0%

Choosing a medical supplier in China requires more than reviewing a catalog or comparing unit prices. Buyers need evidence that products, processes, and records meet the standards relevant to their markets. A polished certificate alone is not enough. Its scope, issuing body, product coverage, and validity should be checked against the exact device and intended use.

This guide explains how to ensure compliance with medical industry standards when assessing suppliers, from initial screening to ongoing quality checks. It covers practical steps such as reviewing quality management system documentation, confirming product testing and traceability, and asking how nonconforming items are handled. Look closely at the details. A batch record, a labeled sample, or a supplier’s response to a corrective-action request can reveal gaps that a sales presentation may not show. Independent audits and qualified regulatory advice can help verify important claims, but no single document guarantees consistent performance. Requirements also vary by device type and destination market, so buyers should confirm current expectations with appropriate experts and authorities. Even careful reviews have limits. A supplier may meet documented requirements today, while changes in materials, production, or subcontractors create new risks tomorrow. The goal is not to assume perfection, but to build a clear, evidence-based process for qualification, monitoring, and follow-up.
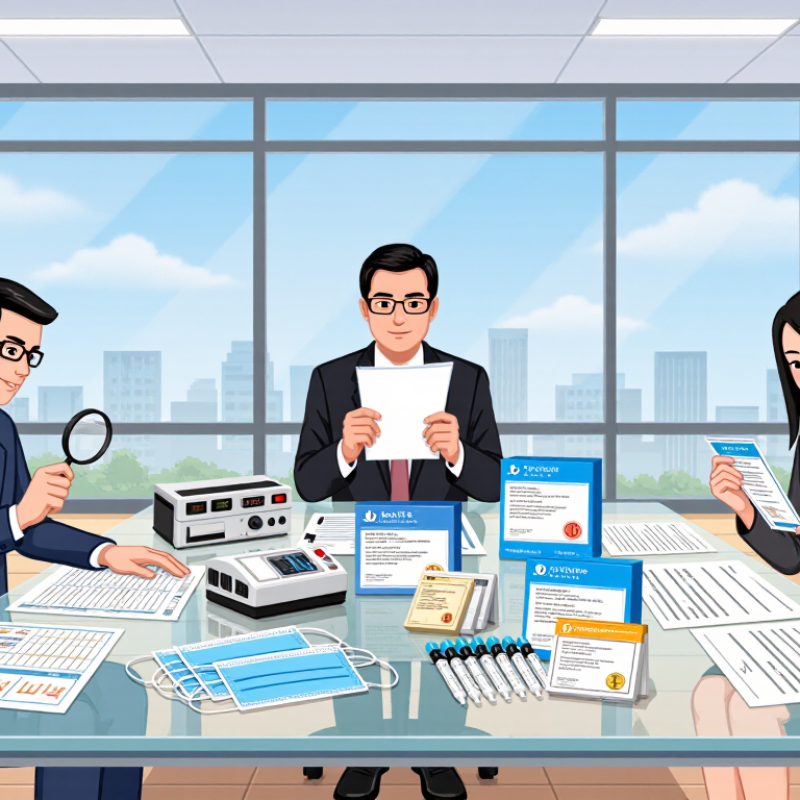
How to Ensure China Medical Suppliers Meet Global Standards?

Understanding the Global Standards for Medical Products

Understanding global standards for medical products means looking beyond a supplier’s certificate. ISO 13485 sets requirements for medical-device quality management, while ISO 14971 guides risk management across a product’s life cycle. Electrical devices may also require testing against relevant IEC 60601 standards. Requirements depend on product type and destination market. A certificate alone does not prove that every batch is safe or consistent.

The World Health Organization estimates that about one in ten medical products in low- and middle-income countries is substandard or falsified. This figure covers varied products and markets; it is not a supplier-specific failure rate. Still, it shows why buyers need evidence. Ask for current certificates, audit scope, test reports, and traceability records. Check whether the documents identify the exact product and manufacturing site. For a practical review, compare incoming inspection results with the supplier’s specifications. A neatly filed report can still miss a real production issue.

Tips: Request a sample batch record and follow one lot from raw-material receipt to final release. Confirm who handles complaints and corrective actions. Keep the questions specific. Review gaps openly; even a strong audit may overlook something.

Mapping Target-Market Regulations and Certification Requirements

Meeting global standards starts with a clear map of the destination market. Requirements can differ by country, product category, intended use, and sales channel. Before evaluating a supplier, define where the device will be sold and how it will be used. A blood pressure monitor, for example, may face different classification and evidence requirements than a sterile surgical instrument.

Ask suppliers for a market-specific compliance file, not a folder of generic certificates. Check whether documents match the exact model, manufacturing site, and intended market. Verify certificate scope, issue dates, and the name of the responsible legal entity. Also review labeling, instructions for use, risk-management records, and evidence supporting performance claims. Details matter. A valid-looking document may cover another product variant.

Build a requirement matrix with local regulatory obligations, recognized standards, registration steps, and renewal dates. Confirm unclear points with qualified regulatory professionals or the relevant authority; rules and accepted evidence can change. During a factory review, trace one finished unit back to its inspection records and material batch. This makes paperwork tangible. Still, a tidy audit cannot prove every process works every day. Keep checking corrective actions, document changes, and post-market responsibilities after the first shipment.

Assessing Supplier Licenses, Facilities, and Production Capabilities

How to Ensure China Medical Suppliers Meet Global Standards?

Assessing Supplier Licenses, Facilities, and Production Capabilities

A supplier’s certificate is a starting point, not proof of consistent performance. Check its business license, medical-device manufacturing authorization, and product registrations against the issuing authority’s records. Confirm that the named legal entity, factory address, product scope, and certificate dates match. The World Health Organization’s Global Atlas of Medical Devices surveyed 194 Member States, highlighting how medical-device regulatory capacity varies widely between countries. Verify approvals for the destination market separately.

Walk the production floor, or arrange an independent audit. Look for clear material-flow routes, controlled storage, equipment maintenance logs, and documented staff training. Ask to trace one finished lot backward to incoming materials and forward to inspection results. ISO’s Survey of Certifications reported more than 30,000 ISO 13485 certificates worldwide in recent editions, but a certificate alone cannot show whether a specific line is controlled well. Details matter.

Production capability should be tested against your real order, not a polished presentation. Review recent output, defect trends, change-control records, and capacity during peak demand. Request sample inspection reports and compare measured results with product specifications. A small pilot order can reveal packaging weaknesses or inconsistent labeling. Audits are imperfect, too; schedules can hide problems. Keep records, revisit findings, and ask suppliers to explain gaps plainly.

Checklist counts show evidence points to verify, not supplier scores or official regulatory totals. Confirm applicable licenses and GMP requirements with the relevant authorities, and assess each supplier’s site-specific documentation and operations.

Verifying Quality Management and Product Compliance

A medical supplier should prove compliance with evidence, not polished presentations. The ISO Survey 2023 recorded over 1.2 million ISO 9001 certificates worldwide. However, ISO 9001 certification alone does not confirm medical device safety. Request an ISO 13485 certificate with its exact product scope, site address, and expiry date. Then compare it with the factory’s quality manual, audit findings, and corrective action records. Small mismatches matter.

On-site verification should follow the product’s real journey. Check incoming material labels, batch records, calibration stickers, and final inspection logs. Review risk management under ISO 14971 and usability controls under IEC 62366 when relevant. Ask how failed units are segregated. Ask again when answers sound memorized. Trace one sample from raw material to shipment. Missing links often appear there.

Product compliance also requires current technical documentation. Review drawings, specifications, test reports, biocompatibility evidence, sterilization validation, and stability data. Match every report to the actual model and manufacturing site.

The World Health Organization reported that about 1.3 billion people, or 16% of the global population, live with significant disability.

That figure reinforces the need for dependable, usable products, not merely compliant paperwork. No audit is perfect. Supplier monitoring should continue through complaints, trend reviews, periodic inspections, and unannounced checks when justified. A certificate can open the door. It cannot replace critical judgment.

Monitoring Supplier Performance and Maintaining Compliance

Medical suppliers must be monitored continuously, not only during qualification. A signed agreement cannot prove ongoing compliance. Set measurable indicators for quality, delivery, documentation, and corrective action response. Review them monthly with clear evidence.

Track batch records, material certificates, inspection results, and temperature logs. Compare received goods with approved specifications before release. During supplier visits, observe warehouse labeling, staff training, equipment calibration, and production controls. Ask practical questions. Do not rely on polished presentations.

A risk-based scorecard helps focus limited audit time. High-risk suppliers may need quarterly reviews, while stable suppliers require less frequent checks. Record every deviation, assign an owner, and set a realistic closure date. Verify that corrective actions work after implementation. A closed form is not proof of improvement.

Communication also matters. Hold scheduled performance meetings and document unresolved concerns. Suppliers should report process changes before shipment, not after a problem appears. No system is flawless. A checklist can miss poor habits on a busy production floor. Independent inspections and random sampling can reveal these gaps. Internal teams should review supplier scores honestly, even when delivery pressure is high. That review may feel uncomfortable. It is often where compliance becomes reliable.

How to Ensure China Medical Suppliers Meet Global Standards? - Monitoring Supplier Performance and Maintaining Compliance
Control Area Global Reference Evidence to Monitor Recommended Control Criterion Review Frequency Escalation Status
Quality Management System ISO 13485:2016 Valid certificate, certification scope, issuing-body details, surveillance-audit records, and certificate expiry date. Certificate must be valid, cover the supplied product and processes, and remain free from unexplained scope gaps. At onboarding and every 6 months Required
Regulatory Authorization Applicable destination-market regulations Manufacturer registration, product listing or authorization, conformity documentation, and authorized representative records where applicable. Documentation must match the legal manufacturer, product model, intended use, and destination market. Before approval and after regulatory change High Risk
Supplier Qualification ISO 13485:2016, Clause 7.4 Initial audit, quality agreement, technical capability review, subcontractor list, and risk classification. Critical suppliers require documented qualification, risk-based approval, and defined re-evaluation criteria. Onboarding and annually Required
Incoming Material Control ISO 13485:2016, Clauses 7.4 and 7.5 Certificates of analysis, incoming inspection records, material specifications, lot numbers, and sampling plans. Materials must meet approved specifications, remain traceable by lot, and be released only after defined acceptance checks. Every shipment or production lot Required
Product Traceability ISO 13485:2016, Clause 7.5.9 Raw-material lots, work orders, production dates, operator records, inspection results, and finished-product serial or lot numbers. Traceability records must link critical materials and production activities to the finished device and distribution records. Every production batch High Risk
Nonconformity and CAPA ISO 13485:2016, Clauses 8.3 and 8.5.2 Nonconformance reports, root-cause analysis, corrective-action plans, due dates, effectiveness checks, and recurrence trends. Critical issues require immediate containment; corrective actions must have verified effectiveness before closure. Monthly and after significant events High Risk
Change Control ISO 13485:2016, Clause 7.3.9 Advance change notifications for materials, tooling, processes, software, site, subcontractors, or manufacturing equipment. No significant change should be implemented without documented impact assessment, approval, validation, and regulatory review where required. Before implementation of each change Required
Delivery Performance Contractual supplier-performance agreement Confirmed-versus-actual delivery dates, shortage records, shipment completeness, and lead-time variation. Recommended internal target: at least 95% on-time and complete delivery, unless a stricter contract target applies. Monthly Monitor
Defect and Complaint Rate ISO 13485:2016, Clause 8.2.2 Incoming defect rate, customer complaints, returned products, failure modes, and trend analysis by lot. Investigate adverse trends, repeated failures, or any defect that may affect safety, performance, or regulatory compliance. Monthly and quarterly trend review High Risk
Sterilization Validation ISO 11135, ISO 11137, or applicable sterilization standard Validation reports, routine monitoring records, environmental controls, biological or dosimetric evidence, and requalification results. Applicable sterilization processes must be validated, routinely monitored, and requalified after defined changes or failures. Per validated cycle and scheduled requalification High Risk
Biocompatibility Evidence ISO 10993 series, where applicable Material composition, biological evaluation plan, test reports, toxicological assessment, and supplier material-change notices. Evidence must reflect the final finished device, intended contact type, duration of contact, and current materials. At design approval and after material change Conditional
Audit and Finding Closure ISO 19011 principles and applicable quality-system requirements Audit reports, finding classification, containment evidence, corrective-action plans, and closure verification. Critical findings require immediate containment; major findings should have approved corrective actions and risk-based closure dates. At least annually for critical suppliers Required
Control criteria are risk-based internal monitoring recommendations. They should be adjusted to the device classification, intended use, applicable destination-market regulations, quality agreement, and validated supplier capabilities.

FAQS

Why is a supplier certificate not enough?

It may not cover the exact product, site, or current production batch. Check its scope and supporting records. Paperwork can look complete.

What documents should buyers request?

Request current certificates, audit details, test reports, and traceability records. Ask for a sample batch record, too.

How can buyers check a batch’s history?

Follow one lot from raw-material receipt to final release. Compare its inspection results with approved specifications. Look for gaps.

Which details matter during a supplier visit?

Check warehouse labels, staff training, equipment calibration, and production controls. Notice what happens on the floor.

How often should suppliers be reviewed?

Review performance monthly. High-risk suppliers may need quarterly checks, while stable suppliers may need fewer audits.

What should a supplier scorecard measure?

Track quality, delivery, documentation, and response times for corrective actions. Use clear evidence for each measure.

How can a buyer tell whether a corrective action worked?

Record the issue, assign an owner, and set a realistic deadline. Verify the change after implementation. A closed form is not proof.

Why use random sampling and independent inspections?

They can reveal problems that checklists or polished presentations miss. No review catches everything. We may miss something, too.

Conclusion

Ensuring that China medical suppliers meet global standards requires a structured and evidence-based evaluation process. Buyers should first identify the international standards relevant to their products, then map the regulations, certification requirements, labeling rules, and documentation expectations of each target market. This foundation helps clarify how to ensure compliance with medical industry standards before supplier selection and contract approval.

The assessment should include verification of supplier licenses, production facilities, technical capabilities, and capacity to maintain consistent quality. Buyers should also review quality management systems, inspection procedures, product testing records, traceability controls, and compliance documentation. After onboarding, supplier performance should be monitored through regular audits, quality reviews, corrective action plans, and updated certification checks. Clear communication, accurate records, and continuous risk assessment can help identify problems early and support reliable, compliant medical product supply.
Amelia

Amelia

Amelia is a seasoned marketing professional with a wealth of expertise in our company’s core offerings. With an unwavering passion for driving growth and innovation, she plays a pivotal role in shaping our marketing strategies and enhancing brand visibility. A key aspect of her responsibilities......